Visible glue lines, uneven trimming, chipped edges, rough corners and feeding problems: what each sign usually means on an edge banding machine, what to check first and when to call service.
Short answer: an edge banding machine usually needs maintenance when you see one of five signs on the finished panel: a visible glue line or weak bond, uneven trimming, chipped or burnt panel edges, rough corners or scraper marks, and panels that feed unevenly. Each sign points to a specific unit of the machine, and most can be traced in a few minutes before they turn into rejected parts or downtime.
Key takeaways
- The finished edge is the best diagnostic tool: inspect the first panels of every shift.
- Glue problems usually come from temperature, a dirty glue system or panel and workshop temperature.
- Trimming, scraping and corner rounding quality depends on sharp tools and clean tracing parts.
- Many feeding problems start with dirty conveyor pads or a pressure beam that needs adjustment.
- Always stop and secure the machine before checking any unit.
How an edge banding line works
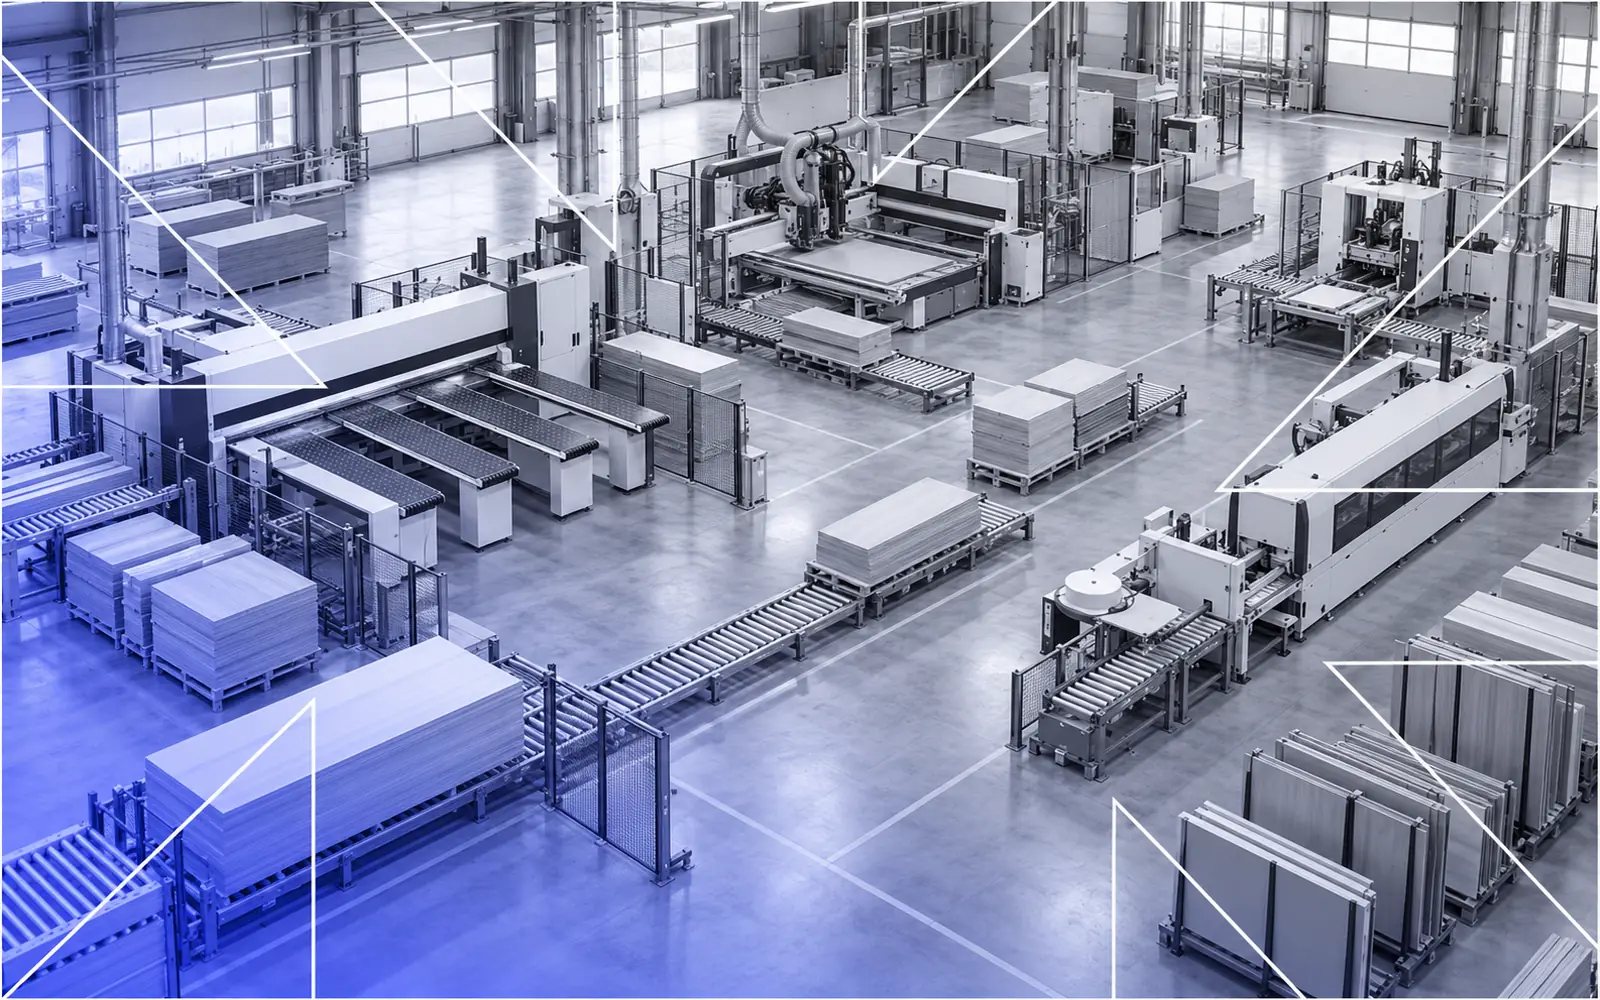
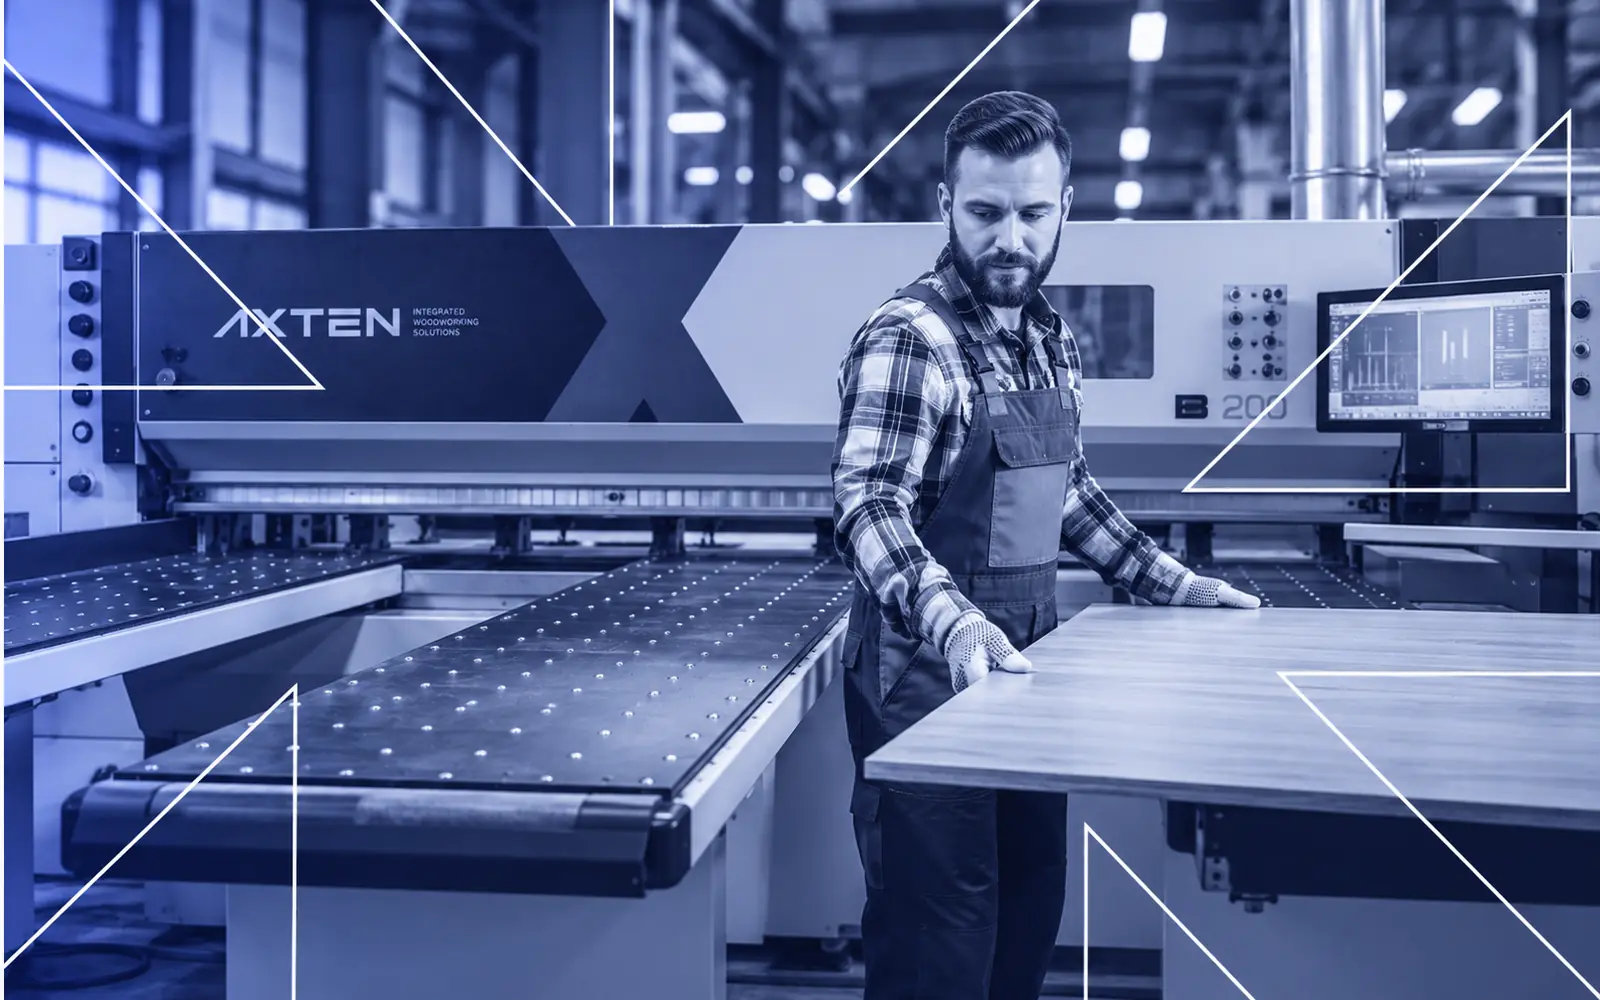
On a fully automatic edge banding machine such as the AXTEA AX-E 300, each panel passes through a sequence of units: pre-milling to create a clean edge, gluing and edge band application, pressure rollers, end trimming, fine trimming, scraping, corner rounding and buffing. A fault in one unit shows up as a specific defect on the finished edge, which is why reading the edge tells you where to look.
1. A visible glue line or weak bond
What you see: a dark line between the panel and the edge band, or an edge band that can be lifted by hand.
Likely causes: glue temperature not reached or not stable, a dirty glue roller or glue pot, too little glue, insufficient pressure from the pressure rollers, or panels and edge band that are too cold. A poor pre-milled edge also reduces bond quality.
Check first: that the glue has reached its working temperature, that the glue system is clean, and that the pressure rollers turn freely and are clean.
2. Uneven trimming or edge overhang
What you see: the edge band stands above or below the panel surface, or the trimmed edge is wavy.
Likely causes: dull fine trimming tools, worn or dirty tracing wheels and copying shoes, or a top pressure beam that does not hold the panel firmly.
Check first: the condition of the trimming cutters and clean the tracing parts.
3. Chipped or burnt panel edges
What you see: small chips in the decorative surface along the edge, or burn marks before the edge band is applied.
Likely causes: dull or damaged pre-milling cutters, an incorrect pre-milling depth, or chips that are not extracted.
Check first: the pre-milling cutters and the dust extraction on that unit.
4. Rough corners or scraper marks
What you see: an uneven radius at the panel corners, steps where the corner rounding unit starts or stops, or marks and glue residue left by the scrapers.
Likely causes: worn corner rounding tools, profile or glue scraper blades that need replacing, or settings that no longer match the edge band thickness.
Check first: scraper blades and corner rounding tools, and the settings for the edge band you are running.
5. Panels feed unevenly or the machine sounds different
What you see or hear: panels that run skewed, slip on the conveyor, stop between units, or a new noise or vibration.
Likely causes: dirty or worn conveyor chain pads, a top pressure beam that needs cleaning or adjustment, or a mechanical problem in the drive.
Check first: clean the conveyor pads and the top pressure beam. If the noise or vibration continues, stop the machine and call service.
Quick reference table
| Sign on the panel | Unit to check |
|---|---|
| Glue line or weak bond | Glue system, pressure rollers, pre-milling |
| Uneven trimming | Fine trimming unit, tracing parts, top pressure beam |
| Chipped or burnt edges | Pre-milling unit and its extraction |
| Rough corners or scraper marks | Corner rounding unit, profile and glue scrapers |
| Uneven feeding or new noise | Conveyor pads, top pressure beam, drive |
When to call service
Call service when a sign returns after cleaning and tool changes, when you hear a new noise or feel vibration, or when the control shows repeated alarms. AXTEA usually starts with a remote connection through its call center; this often resolves the issue outright and otherwise tells the technician which parts to bring. For routine checks, see our daily and weekly maintenance checklist.
Frequently asked questions
Why is there a visible glue line on my edge banded panels?
Most often the glue has not reached working temperature, the glue system is dirty, there is not enough pressure, or the panels and edge band are too cold. A poor pre-milled edge can also cause it.
How often should edge banding tools be checked?
Inspect the finished edge every shift and check pre-milling, trimming, scraping and corner rounding tools at least weekly, more often in high-volume production.
What causes chipping on the panel edge before edge banding?
Usually dull or damaged pre-milling cutters, an incorrect pre-milling depth or poor chip extraction at the pre-milling unit.
Do you service edge banding machines from other brands?
Yes. AXTEA supports machines across a wide range of brands and models. Send us the make, model and year and we will confirm what we can cover.
Last updated: